Electro discharge machining
 Call Kai
 Learn
 Practice Test
 Spaced Repetition
 Match
 Flashcards
 Knowt Play
1/10

There's no tags or description
Looks like no tags are added yet.
11 Terms
What is electro discharge machining (EDM) and how does it work?
EDM is an advanced machining technologies that focuses on the subtraction of material to create a final shape
It works when two electrodes the tool and workpiece are placed into a dielectric fluid and submitted to high voltage and separated by a gap. The tool is then moved toward the workpiece and if the gap is small enough an electrical current occurs by the discharge of the capacitor which creates a spark which in turn creates a crater on the workpiece and on the tool. Dielectric is contaminated with debris and so the tool is moved away so the dielectric can be cleaned.

the trade off between efficiency vs quality
Energy output is controlled by the voltage, current and time on/off to charge/ discharge the capacitor
Higher energy creates:
bigger craters
bigger spark gap between the electrodes and machined surface
higher removal rate
rougher surface (higher Ra)
what is Ra?
It is used to measure roughness and takes into account the average displacement of peak and trough of the craters, the higher the Ra the more rough. Can have a near mirror finish at 0.02 micrometres or a rough surface at 10 micrometres
What are the 4 typical uses (processes) of electro discharge machining?
Wire EDM
Die sinking EDM
EDM drilling
EDM milling
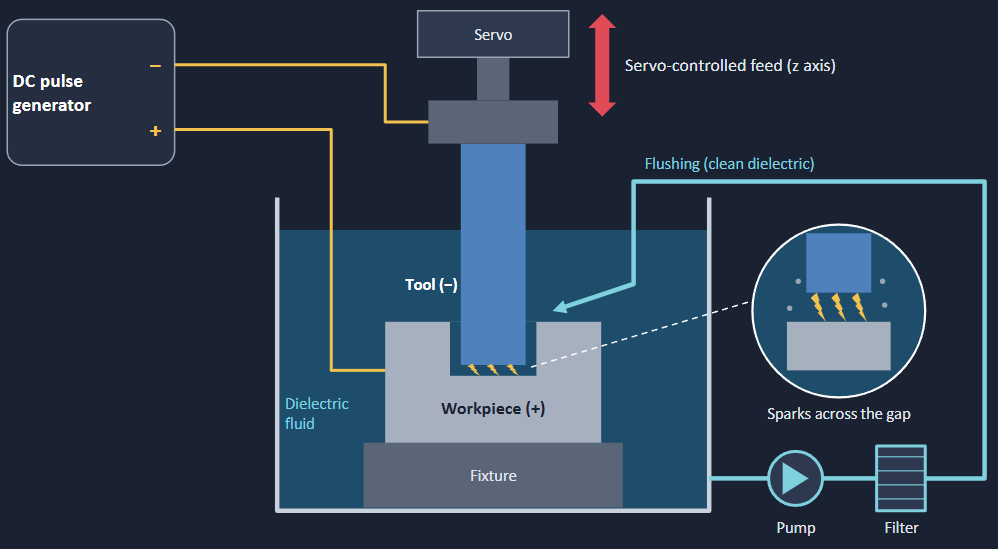
What is die sinking EDM
A tool mainly made out of graphite or copper, tungsten or tungsten carbide moved in the Z axis (up and down) and acts like a punch to create a negative version on the workpiece.
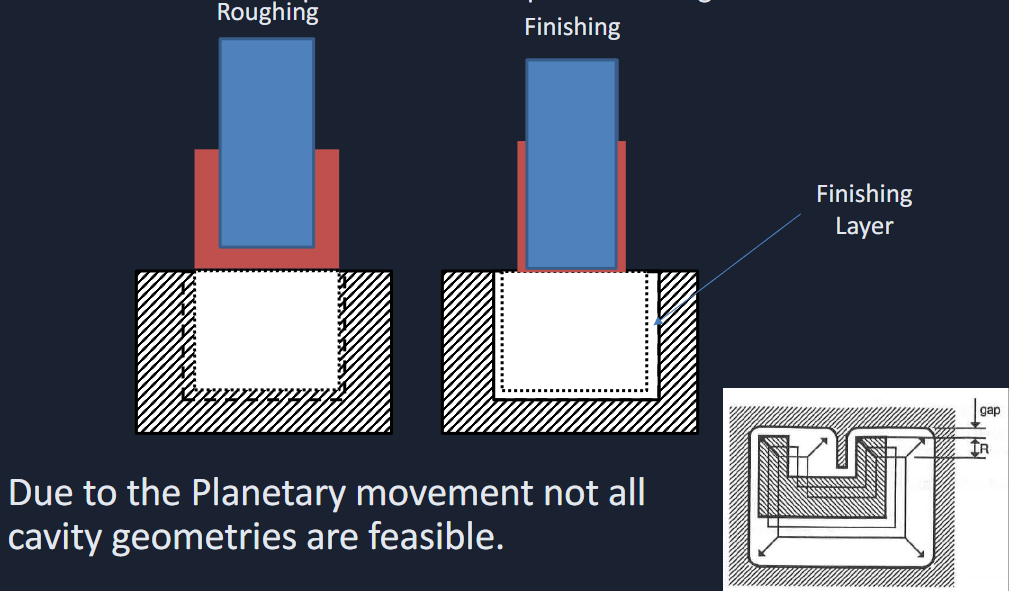
to produce a part of good quality in a short period the roughing, finishing method is used whereby high energy is used to remove a load of material at first leaving some material left over so it can be removed by the lower energy finishing to create a smooth surface. As the spark gap is smaller at lower energies the tool needs to be bigger (not always possible as it depends on the shape) or the tool needs to be moved around in the shape of the component.
advantages
high quality surfaces
any conductive material, regardless of hardness
limitations
tools can be difficult to produce
tools can be difficult to control in small geometries
slow process and is expensive
tool also wears out as well from sparks
How to control die electric flushing on die sinking?

Wire electro discharge machining
wire is fed into workpiece and the sparks cut though the workpiece by electrical discharges between the wire and workpiece. The wire is on a supply and take up wheel so new wire is fed though and therefore does not wear out and snap.
advantages
no wear compensation needed as wire is constantly renewed
easy flushing bought by movement of wire
high quality surfaces
any conductive material regardless of hardness
main limitation
wire control as its in tension
can only machine conductive materials
produces mainly 2D shapes
corner diameters limited by wire diameter + spark gap
uses: gears, fly fishing lines
Think about the wire EDM strategy used for producing a die
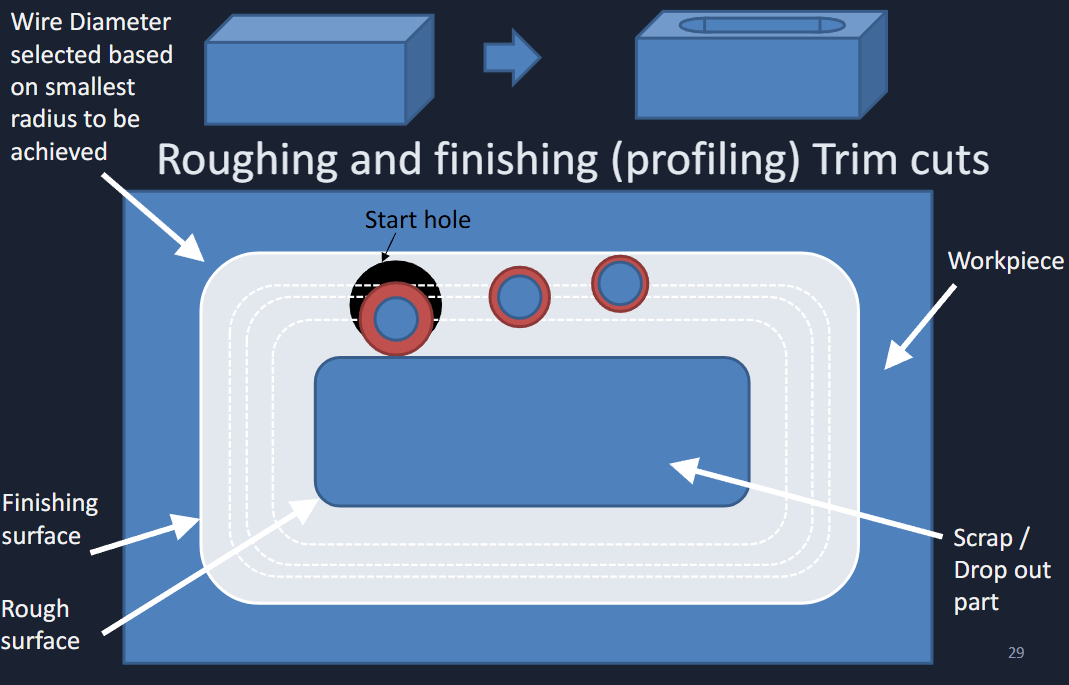
Think about the wire EDM strategy used for producing a punch

EDM drilling
Can produce very deep holes of an aspect ratio over 100 meaning the length of the rod can be over 100 times the diameter. regular drilling cannot do this due to poor thermal removal and lesser material removal.
material is flushed though hollow electrode

EDM milling
like drilling a small rotating cylindrical electrode is used but with a cutting strategy similar to standard milling and can produce complex 3D shapes with features down to 5 micrometres
It has good flushing leading to improved geometry but is extremely time consuming and typically only used for cavities smaller than 100mm²
Material removal rate table example
