AUTOTECH 3MP3:Manufacturing Processes and Systems Test 2
 Call Kai
 Learn
 Practice Test
 Spaced Repetition
 Match
 Flashcards
 Knowt Play
1/11

There's no tags or description
Looks like no tags are added yet.
12 Terms
Compare between shielded metal arc welding and gas tungsten arc welding in terms of heat source, protection, electrode type, rate of heat input, advantages, and limitation
With the aid of proper schematics, describe how metal powder is fabricated.
An engine lathe is used to turn a cylindrical work part 150 mm in diameter by 500 mm long. Cutting speed = 2.50 m/s, feed = 0.30 mm/rev, and depth of cut = 3.0 mm. Determine (a) cutting time and (b) metal removal rate
A slab-milling operation takes place on a 300-mm long and 40-mm wide workpiece. A 75-mm diameter cutter with 10 teeth is used. Assume that the cutter travel distance is 20 mm. If the feed per tooth is 0.2 mm/tooth and the cutting speed is 0.75 m/s, calculate the machining time and metal removal rate for removing 6 mm from the surface of the part
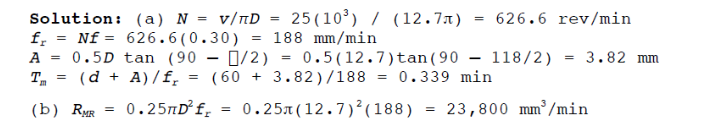
A drilling operation is performed on a steel part using a 12.7-mm-diameter twist drill with point angle = 118°. The hole is a blind hole with a depth of 60 mm. Cutting speed = 15 m/min and feed = 0.20 mm/rev. Determine (a) cutting time of the operation and (b) metal removal rate after the drill bit reaches full diameter
With the aid of a schematic, describe what HAZ (Heat Affected Zone) is in a weldment.Comment how the magnitude of HAZ affects the mechanical properties of the weldme
In a turning operation, spindle speed is set to provide a cutting speed of 1.8 m/s. The feed and depth of cut are 0.30 mm/rev and 2.6 mm, respectively. The tool rake angle is 8°. After the cut, the deformed chip thickness is measured to be 0.49 mm. Determine (a)shear plane angle, (b) shear strain, and (c) material removal rate. Use the orthogonal cutting model as an approximation of the turning process

The cutting force and thrust force in an orthogonal cutting operation are 1470 N and 1589 N, respectively. The rake angle = 5°, the width of the cut = 5.0 mm, the chip thickness before the cut = 0.6, and the chip thickness ratio = 0.38. Determine (a) the shear strength of the work material and (b) the coefficient of friction in the operation

A cylindrical workpiece 200 mm in diameter and 700 mm long is to be turned in an engine lathe. Cutting speed = 2.30 m/s, feed = 0.32 mm/rev, and depth of cut = 1.80 mm. Determine (a) cutting time, and (b) metal removal rate

A drilling operation is to be performed with a 12.7 mm diameter twist drill in a steel workpiece. The hole is a blind hole at a depth of 60 mm and the point angle is 118°. The cutting speed is 25 m/min and the feed is 0.30 mm/rev. Determine (a) the cutting time to complete the drilling operation, and (b) metal removal rate during the operation, after the drill bit reaches full diameter
Tool life tests in turning yield the following data: (1) when cutting speed is 100 m/min, tool life is 10 min; (2) when cutting speed is 75 m/min, tool life is 30 min. (a) Determine the n and C values in the Taylor tool life equation. Based on your equation, compute (b) the tool life for a speed of 110 m/min, and (c) the speed corresponding to a tool life of 15 min.

In a production turning operation, the workpiece is 125 mm in diameter and 300 mm long. A feed of 0.225 mm/rev is used in the operation. If cutting speed = 3.0 m/s, the tool must be changed every 5 workpieces; but if cutting speed = 2.0 m/s, the tool can be used to produce 25 pieces between tool changes. Determine the Taylor tool life equation for this job.
