IME 1143 Midterm
 Call Kai
 Learn
 Practice Test
 Spaced Repetition
 Match
 Flashcards
 Knowt Play
1/94

There's no tags or description
Looks like no tags are added yet.
95 Terms
traditional machining processes
turning, milling, drilling, sawing, broaching
describe the traditional milling process
multi-tooth rotating cutter removes material while along various axes with respect to the workpiece, one of the most versatile machining processes
traditional milling machine axes
basic CNC milling machines have 3
traditional milling cutters
multi-tooth tool that produces multiple chips in one revolution
traditional drilling process
creation of cylindrical holes with a twist of drill, one of the most common machining processes to produce holes
what type of tools can drilling be performed with
drill presses, hand drills, mills, lathes
twist drill charactertistics (how they’re held, sizing)
commonly held in drill chucks, come in four different sizes (metric, fractional, letter, number)
traditional sawing process
cutting tool is a blade with a series of teeth where each tooth removes a small amount of material with each stroke or movement, can be used for all metallic and nonmetallic materials, can produce various shapes
characteristics of traditional sawing process
tooth in the saw provides wide kerf —> blade moves freely in workpiece —> reduces binding or frictional resistance —> reduce heat generated, different blade depending on softness and hardness of materiald
different types of saws
band (continuous, long, flexible blades that produces a continuous cutting action — vertical or horizontal), circular/cold (create precise, burr-free cuts and corners w. out sparks or generating heat — typically have a coolant delivery system), abrasive (AKA cutoff or metal chop, usually cut steel or stainless steel, think abrasive disk spins to cut the metal, disk must be replaced regularly, inexpensive comp to band saws)
traditional broaching process
performed on a broaching machine or arbor press, cutting tool itself is called a broach, produces complex shapes with sharp internal corners, used in production to finish an entire surface in a single pass with special shaped holes, splines, flat surfaces, & complex shapes that can’t be achieved by milling or turning
characteristics of traditional broaching process (features about the tool, internal broaching, the finished surface)
internal broaching requires an existing hole on the piece, each tooth stands slightly higher than the last —> creates chip thickness, machined surface is always the inverse of the broach’s profile (frontal contour of the teeth determines the shape of the machined surface)
general charactertistics of cutting tools
creates shear stress to remove a chip from the workpiece, all have rake angles, lead angles, a corner radius, and clearance angles, has to be harder than the workpiece
different cutting tool materials
high carbon steel, high speed steel, carbide
high carbon steel
for less expensive drills, taps, and reamers, very shallow hardening (outside will harden but inside will still be soft), rarely used for single point cutting tools or milling tools
high speed steel
retain surface hardness at temperatures up to 1100 degrees Fahrenheit, deep hardening
carbide
industry standard, produces the fastest cutting speed —> good surface finish, high degree of hardness, retain temperatures up to 1400 degrees Fahrenheit, different types (straight tungsten, alloyed, coated)
rake angle
slope of the cutting tool’s face relative to the workpiece surface, inclination increases or diminishes the keenness or bluntness of the edge (1= negative rake, 2 = neutral rake, 3 = positive rake), dictates how the chip flows across the tool
lead angle
the angle between the cutting edge of the tool and the workpiece, more lead = easier to cut
corner radius
strengthens the cutting edge —> improves finish and influences tool life, too large of a radius —> increase radial forces and induces chatter, too small of a nose radius —> premature chipping or prevent proper distribution of heat —> break down the properties of the cutting tool material
clearance angle
primary clearance is directly below the cutting edge (prevents the cutter/tool from rubbing on the workpiece), secondary clearance is on the tooth of the milling cutter or the shank of the single point tool (has to be large enough to clear the workpiece and permit chips to escape)
maching processes basic variables
cutting speed, chip load, depth of cut
cutting speed
AKA surface speed, speed between the tool and workpiece, used to calculate the spindle’s RPM, measured in ft/min
chip load
cross sectional size of chip being sheared off workpiece, thickness of material being sliced off by a single tooth of the tool, measured in in/rev or in/tooth
depth of cut
thickness of material removed by a cutting tool from a workpiece in a single pass, overall size of the channel the tool is cutting in to the workpiece, determined using the cross slide on the lathe, measured in m
turning
part is rotated while it’s being machined, one of the most basic processes, changes the diameter of the piece
facing
produces flat surface at the end of the part, changes the length of the part
conventional milling
cutter rotates in the opposite direction to the feed movement of the work piece, creates thin to thick chip, rougher/poorer surface finish compared to climb milling
climb milling
cutter rotates in the same direction as the feed movement of the workpiece, creates thick to thin chips, smoother surface finish with less chatter, preferred direction of cutting in a CNC mill, uses less horse power
face milling
machining a flat surface normal (90 degrees) to the axis of the rotating cutter, typically a cutter w/ a larger diameter intended to make flat faces on the workpiece
peripheral milling
AKA end milling or contouring, axis of the cutter rotation is parallel to the workpiece’s surface being generated
how is depth of cut calculated on a lathe
it’s the radial thickness of material removed per pass, so half the total change in diameter — basically half the amount of whatever measurement is on the cross slide of the lathe
what usually holds the workpiece in a lathe
3-jaw chuck
purpose of cutting fluid
used during turning and milling, reduces friction and heat, different types include oil, emulsion, gas, and paste
why is it important to spot/center before drilling
ensure the tool does not go off target and ensure a clean entry chamfer
how to read a drill and tap chart
find the column containing the required thread size, find the row with the corresponding drill size (should be around 75% of the full thread depth)
reaming
process that slightly enlarges (more like smooths and sizes) a pre-existing hole with a tight tolerance diameter, tool consists of a central shaft with several cutting edges that remove a little bit of a material
boring
an operation in which a hole is enlarged to a precise value with a single point cutting tool, on lathe or mill

the ½ refers to
the nominal thread size (major diameter)
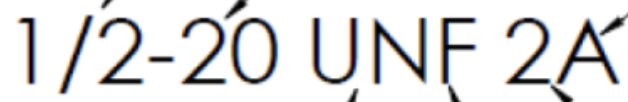
the 20 refers to
the threads per inch (pitch is the inverse of that value)

the UN refers to
the form — unified national

the F refers to
the series (fine or course)

the 2 refers to
the class (1 = loose, 2= normal, 3 = higher tolerance)

the A refers to
the placement (A = external, B = internal)
resolution of the dial calipiers used in lab
.001
rule of 10
a measuring instrument should be at least ten times more accurate (have 10 times better resolution) than the tolerance range of the part being measured
accuracy
the degree to which the measured value agrees with the true value or against the standard
precision
repeatability, achieved by selecting the proper instrument technology for the application
height gage
applies basic design principles of vernier caliper gages, surface plate functions as a datum reference plane for second contact member
fixed gage
embody the direct or reverse physical replica of the object to be dimensioned, two different types — master gages (the nominal conditions) and limit gages (the limit conditions)
CMM
coordinate measuring machines, stationary instruments that employ their own standards for obtaining dimension measurements at a high degree of accuracy
different types of CMM sensors
video, tactile, laser
video CMM sensor
systems use cameras and image processing to perform inspection of parts (counting objects, reading serial numbers, searching for defects), strengths include edge detection, fast data acquisition, non-contact; weaknesses include limited surface information, feature must be illuminated and imaged
tactile CMM sensor
strengths include that they have a very general purpose, more surface information, access to internal internal features; weaknesses include slower data acquisition, requires physical contact
laser CMM sensor
uses a laser to perform 3D scans to create a surface model, strengths include surface profiling, fast data acquisition, and non-contact; weaknesses include surface dependent performance and working distance
indicators
sense displacement, meant to detect variations in a specific distance
dial indicator
senses measuring distance variations that are in the axial direction of the measuring spindle, two different types — balanced and continuous
test indicator
used to sense displacement that occur in a direction essentially perpendicular to the spindle’s contact point, establishes parallelism or perpendicularity
when to use abrasive machining over traditional processes
when basic machining processes cannot produce the required dimensional accuracy or surface finish, workpiece could be too hard or brittle for basic machining processes
abrasive machining processes
uses abrasive grains to remove small amounts of material from a surface by a cutting process that produces tiny chips, can be used to also hone, lap, buff, and polish work pieces
grinding process
most common abrasive machining process, uses a single abrasive grain as the cutting tool to remove material from the workpiece
grit number
used to specify the size of the abrasive particle (how many abrasive particles can fit in a linear inch), smaller the grain size the larger the number
different types of grinding
surface, cylindrical, centerless, CNC, abrasive belt
surface grinding
the most common, generally involves the grinding of flat surfaces, workpiece held on a magnetic chuck
cylindrical grinding
external cylindrical surfaces and shoulders of workpieces are ground (AKA center-type grinding), rotating` grinding wheel travels down the length of the rotating cylindrical workpiece
centerless grinding
grinding cylindrical surfaces where the workpiece is not supported by centers or chucks but by a blade, ability to grind the entire outside diameter in one operation
CNC grinding
grinding wheel is trued to the shape of the feature being ground into the part
abrasive belt grinding
used in machining industry for deburring, removing stock, cleaning up of metal surfaces, grinding welds, robotic grinding
honing
a finishing process involving a rotating tool carrying abrasives removes metal from the surface of a workpiece’s bore, performed on internal cylinder walls using a combined rotating and reciprocating motion, tight tolerance, eliminates inaccuracies from previous machining operations, achieves final dimensional size, generates high quality surface finishes (how all hydraulic cylinders are honed)
abrasive flow machining
abrasive media flows through the workpiece, hydraulic ram forces the media through the workpiece, molds itself to the shape of the workpiece and removes any raised features on the surface
lapping
the removal of material to produce an accurate smooth, matte or polished surface, used for finishing flat, cylindrical, or curved surfaces, abrasive particles mixed with a water or oil base (slurry) then placed on a rotating motorized platform, produces the best dimensional accuracy
non-traditional machining processes
the processes that do not use shear stress as their primary source of energy to remove material, higher energy and slower throughputs compared to the traditional machining processes, use when traditional methods are impractical, incapable, or uneconomical
categories of non-traditional machining processes
mechanical, electrical, thermal, chemical
heat affected zone
area of material that does not melt during machining but has its mechanical properties altered by high heat exposure
chemical machining/milling
components produced by the etching technique using a wide array of metal and alloys, voids burrs, no mechanical stresses or HAZ, for thin metals and foils & parts with very precise and intricate designs, two different systems are chemical or photochemical
electrical discharge machining
AKA machining via sparks, uses electrical pulses to produce tiny, highly focused sparks that erode metal smoothly and precisely, spark discharge creates thermal energy that erodes electrically conductive materials, material removal is independent of work piece hardness
sinker die EDM
pre-shaped custom electrode machined into the exact mirror image of the desired cavity, electrode and metal workpiece are submerged into a non-conductive dielectric fluid, electrode lowered toward metal until spark forms, electrical discharge melts/vaporizes portion of the workpiece, recast layer has a HAZ
wire EDM
ultra thin wire produces high-frequency electrical sparks that melt and vaporize tiny amounts of metal, contains a HAZ
EDM advantages
no cutting forces, high aspect ratios, intricate cavities, unaffected by material hardness
EDM disadvantages
electrically conductive workpiece required, low MRR, recast and HAZ, consumable electrode, high capital cost, slow
laser cutting
process of vaporizing material in a very small, well-defined area, laser is a single point cutting source with a very small point (small cut widths), process used to cut materials, mark surfaces, weld, and heat in exact locations
laser cutting advantages
smaller HAZ compared to other thermal cutting methods, no limit to the cutting path, forceless (fragile or flimsy parts can be cut with no support), laser is always “sharp” so hard, abrasive, or sticky materials can be cut still, high speeds
electromechanical machining
uses electrical energy to remove material, electrolytic cell created in an electrolyte (tool is the cathode and workpiece is the anode), low voltage current passed through the cell, dissolving away the material to be removed, shape of the cathode (tool) determines the final shape of the workpiece
ECM advantages
speed of machining does not depend on the hardness of the workpiece material, tool does not wear, no stresses or HAZ produced, burr-free (super smooth surface finish), high accuracy (tight tolerance)
ECM disadvantages
higher cost, electrolyte can cause corrosion of the equipment, takes up a lot of floor space, noly electrically conductive materials can be machined, not environmentally friendly
ultrasonic machining (USM)
mechanical material removal process used to machine holes and cavities in hard or brittle workpieces (like glass), uses shaped tools (creates mirrored image in the workpiece), high frequency mechanical motion, and an abrasive slurry to erode away the workpiece, can machine all materials harder than Rockwell 45 HRc
advantages of ultrasonic machining
capable of machining brittle and hard materials with high precision, machine conductive and non-conductive materials, does not leave a HAZ, absence of burrs in the process —> less finishing processes and good surface finishes overall
USM disadvantages
metal removal is slow due to micro chipping or erosion mechanism, can only machine workpieces that have a rockwell hardness > 45 HRc, abrasive slurry can’t be reused, tool wears fast, uneconomical b/c of tooling design, difficult to drill deep holes b/c of slurry delivery
waterjet machining
a mechanical material removal process capable of slicing into metal or other materials using a jet or water at high velocity and pressure, cutter is connected to a high-pressure water pump, water fed through a small orifice where it mixes with an abrasive, ejected out of nozzle and erodes away the material, cuts diverse range of materials (bread to titanium)
advtanges of waterjet machining
able to cut almost any type of material (does not work for highly brittle materials like tempered glass and ceramics), produces no hazardous waste, no HAZ, can cut through thicker materials and materials that do not melt, parts can be cut from sheetmetal or plate material and require no special clamps, fixtures, or tool changes
disadvantges of waterject machining
cannot create blind cut sor features, can create small indentations where the stream of water begins and ends, kerf width is between .02 and .04 inches, abrasive garnet cannot be reused
kerf
the thickness of material that the jet removes
producting planning
the nervous system of the manufacturing operation, includes planning, routing, scheduling, dispatching, and follow up in the production process — for the entire company
manufacturing routing
for a single part and all the operations that it goes through
operation sheet
detailed instructions on performing a specific manufacturing step, for a single operation